31. to reduce the effect of magnetic arc blow which alternative can be used.\na. increase welding…
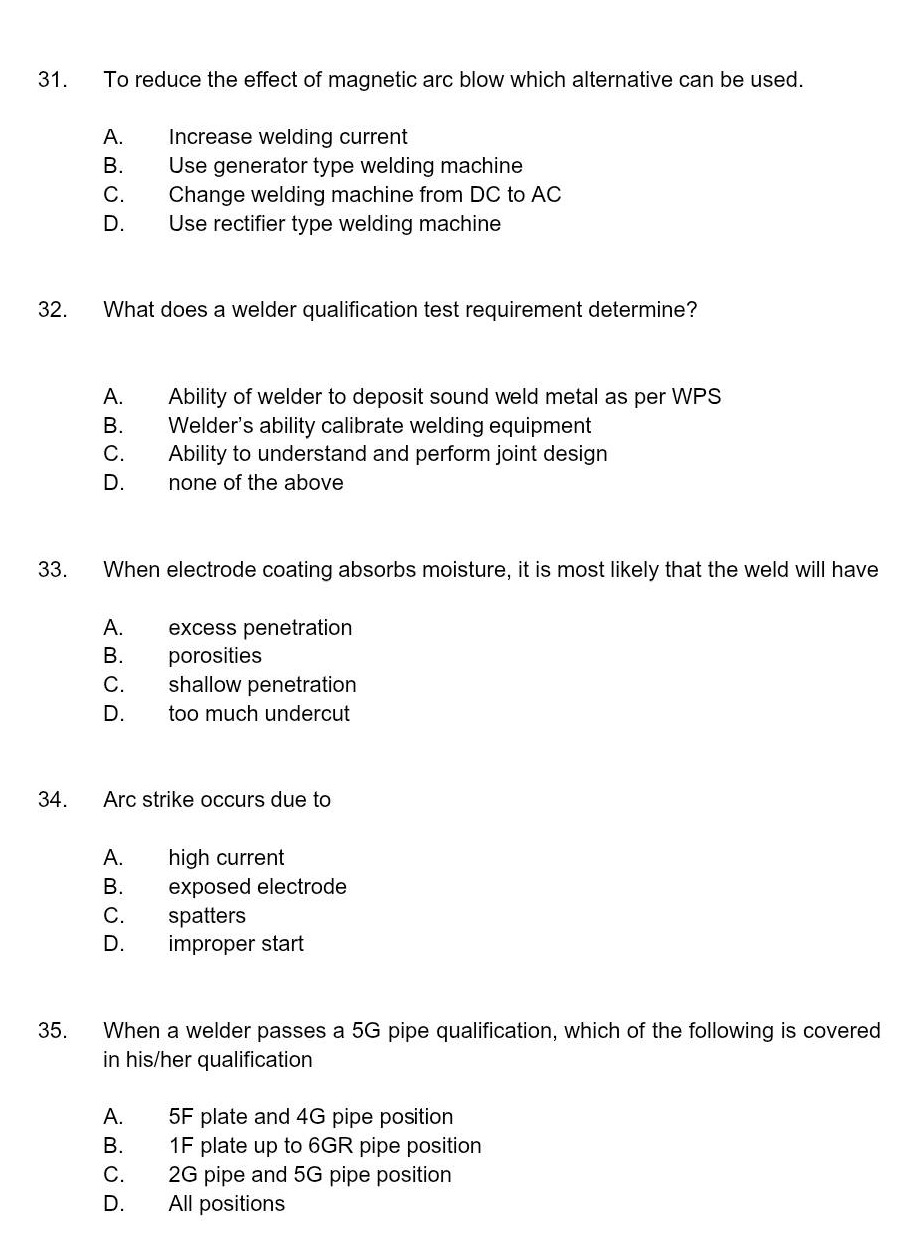
31. to reduce the effect of magnetic arc blow which alternative can be used.\na. increase welding current\nb. use generator type welding machine\nc. change welding machine from dc to ac\nd. use rectifier type welding machine\n32. what does a welder qualification test requirement determine?\na. ability of welder to deposit sound weld metal as per wps\nb. welders ability calibrate welding equipment\nc. ability to understand and perform joint design\nd. none of the above\n33. when electrode coating absorbs moisture, it is most likely that the weld will have\na. excess penetration\nb. porosities\nc. shallow penetration\nd. too much undercut\n34. arc strike occurs due to\na. high current\nb. exposed electrode\nc. spatters\nd. improper start\n35. when a welder passes a 5g pipe qualification, which of the following is covered in his/her qualification\na. 5f plate and 4g pipe position\nb. 1f plate up to 6gr pipe position\nc. 2g pipe and 5g pipe position\nd. all positions
Answer
Brief Explanations:
- For question 31, changing from DC to AC welding machine can reduce magnetic arc blow as AC current has a changing direction which mitigates the magnetic - related issues.
- For question 32, a welder qualification test checks the welder's ability to deposit sound weld metal as per the Welding Procedure Specification (WPS).
- For question 33, when electrode coating absorbs moisture, it releases gases during welding which can cause porosities in the weld.
- For question 34, arc strike occurs mainly due to an improper start of the welding process.
- For question 35, passing a 5G pipe qualification covers the 5G pipe position and also the 2G pipe position as part of the scope.
Answer:
- C. Change welding machine from DC to AC
- A. Ability of welder to deposit sound weld metal as per WPS
- B. porosities
- D. improper start
- C. 2G pipe and 5G pipe position